Slider Image
Slider Thumb

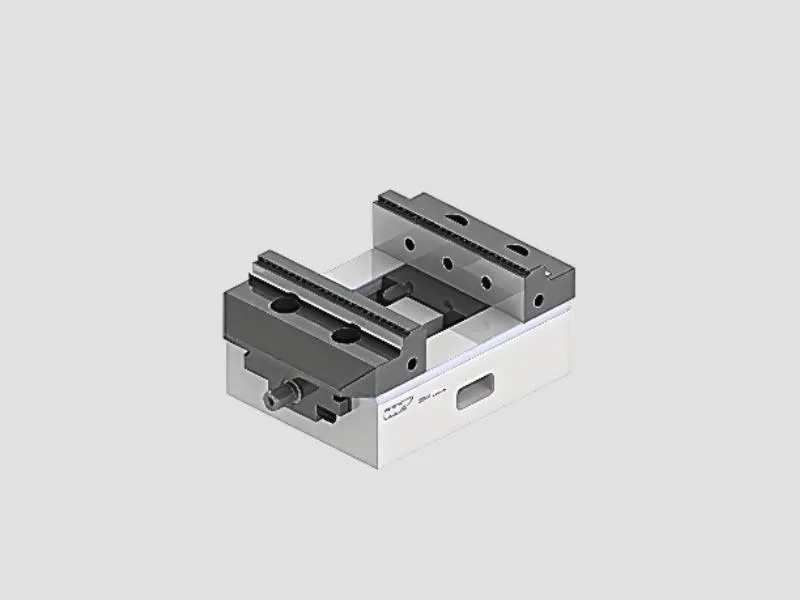
Clamping systems can be categorized into various types, including mechanical vices, pneumatic clamps, magnetic fixtures, and hydraulic chucks. The choice of clamping device depends on several factors, including the material of the workpiece, the forces applied during machining, and the type of machining operation. Mechanical vices are commonly used for their simplicity and versatility, while more specialized systems, like hydraulic or pneumatic clamps, offer high clamping forces with minimal operator intervention. Magnetic clamps are often used for non-ferrous materials or for high-precision applications, while hydraulic chucks provide a strong and evenly distributed clamping force for heavy-duty machining.

Cash,Cheque,Demand Draft,UPI, NEFT

Key Attributes
Industry-specific Attributes
  • Values 50°C – 500°C (depending on material and operational conditions).
  • Values 5 kg – 10,000 kg (depends on the type of clamping system, with hydraulic and magnetic systems typically handling higher loads).
  • Material Compatibility Steel, Aluminum, Cast Iron, Plastic, Titanium, Non-ferrous Metals, Ceramic, Composite Materials.
  • Clamping Force 50 N – 100,000 N (depending on the device type and application)
  • Clamping Range 5 mm – 1,000 mm (depending on the size of the workpiece and clamping device).
Other Attributes
  • Mounting Method Direct Mount, Rotary Table, Turntable, Adjustable Fixture, Pneumatic Mount, Magnetic Base, T-slot Mounting.
  • Adjustment Mechanism Manual Adjustment, Hydraulic Adjustment, Pneumatic Adjustment, Quick-release, Fine-tuning Adjustment.
  • Compatibility with Machines CNC Machines, Milling Machines, Lathe Machines, Grinding Machines, Welding Machines, Turning Machines, Drilling Machines.
  • Surface Protection Zinc-plated, Chrome-plated, Nickel-coated, Powder-coated, Anti-corrosion treated, Ceramic Coated.
Slider Image
Slider Thumb

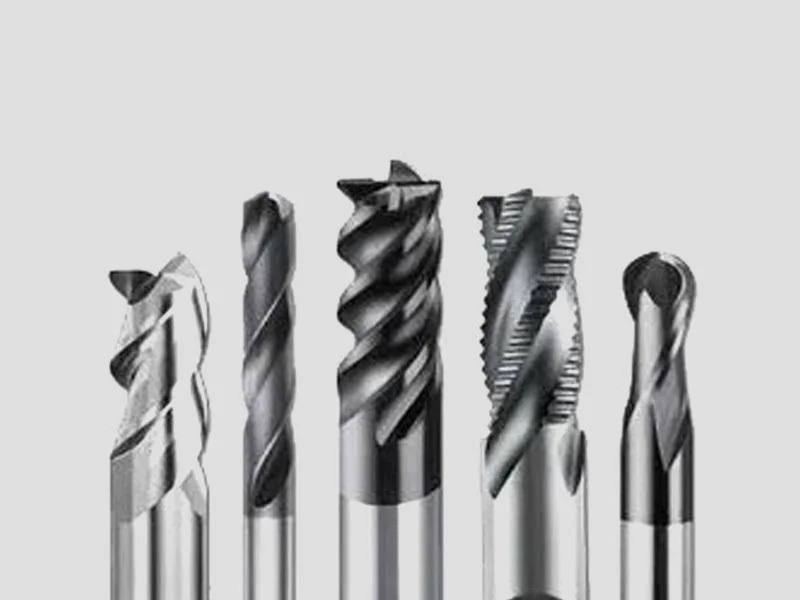
End mill cutters are a fundamental tool used in milling machines, enabling the shaping and finishing of materials such as metals, plastics, and composites. The versatility of end mills allows for a wide range of milling operations, such as face milling, slot milling, and profile cutting. Unlike drill bits, which only cut on the tip, end mill cutters have cutting edges on the side as well, providing lateral cutting action. This ability makes them suitable for more complex operations, including those that require precise and smooth surface finishes. The most common material for end mill cutters is high-speed steel (HSS), though carbide is often preferred in high-performance applications due to its superior hardness and resistance to wear and heat. 

Cash,Cheque,Demand Draft,UPI, NEFT

Key Attributes
Industry-specific Attributes
  • Diameter Ranges from a few millimeters (e.g., 1mm) to several inches (e.g., 25mm or more), depending on the application.
  • Length Typically ranges from 1 inch (25mm) to several inches (up to 10 inches or more) based on tool design and workpiece depth.
  • Flute Count Usually between 2 and 8 flutes; more flutes provide better surface finish, while fewer flutes are suitable for higher material removal rates.
  • Shank Type Common types include Weldon shank, straight shank, or clamping shank, with each offering different methods of tool attachment.
  • Coating Type Titanium Nitride (TiN), Titanium Aluminum Nitride (TiAlN), or Diamond-like Carbon (DLC) are common coatings that improve wear resistance and reduce friction.
Other Attributes
  • Material Type High-speed steel (HSS), carbide, cobalt, or carbide-tipped, with carbide being most suitable for hard materials and high-speed operations.
  • Cutting Edge Style Square end (for flat-bottom cuts), ball end (for 3D contouring), corner radius (for rounded corners), or roughing end mills (for fast material removal).
  • Chip Removal System Some end mills include internal coolant channels or special flute designs to improve chip removal and reduce heat.
  • Tolerance Tolerance can vary, with precision cutters offering tighter tolerances of ±0.0001 inches, while general-purpose tools may have tolerances of ±0.001 inches.
  • Surface Finish End mills with more flutes tend to offer better surface finishes, while roughing end mills provide a more aggressive cut but at a rougher finish.
Slider Image
Slider Thumb

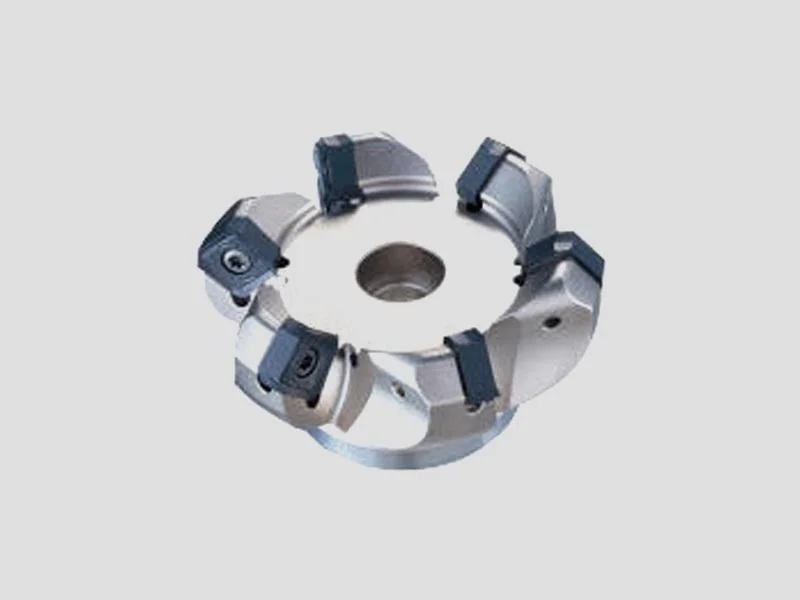
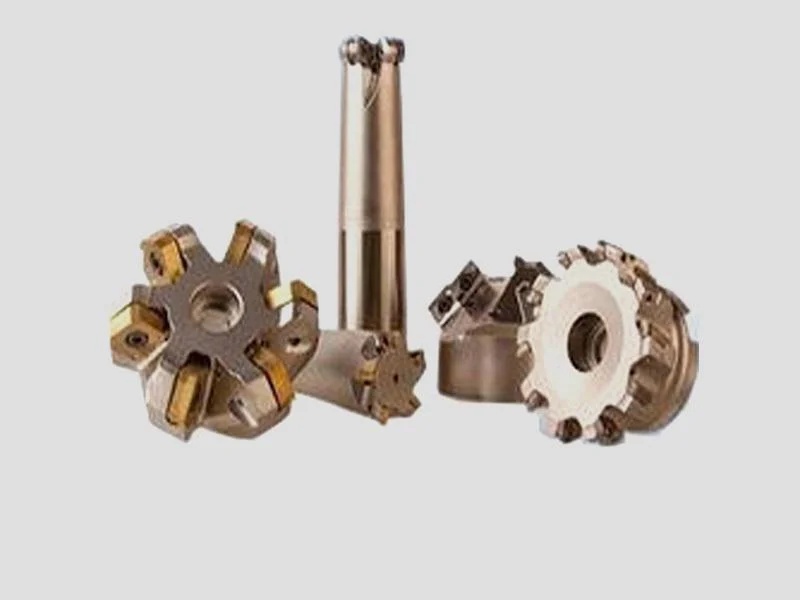
Discover the Indexable Milling Tool for Heavy Duty Metal Processing designed for demanding industrial machining operations. This tool is widely used in CNC machining centers, fabrication units, and engineering workshops for efficient and precise material removal. The replaceable insert design helps reduce downtime and lowers overall tooling costs. It is suitable for machining steel, cast iron, and various alloy metals while maintaining consistent accuracy. The tool delivers stable cutting performance even under high load and continuous operation conditions. Multiple sizes and insert options are available to suit different machining needs. Customization can be provided based on specific applications and production volumes. All products are sourced from verified manufacturers and reliable suppliers. Quality standards are maintained to ensure long service life and dependable performance. Competitive pricing and bulk order support make it ideal for industrial buyers.

Cash,Cheque,Demand Draft,UPI, NEFT

Key Attributes
Industry-specific Attributes
  • Material Carbide, Ceramic, Cermet, High-Speed Steel (HSS)
  • Insert Geometry Square, Round, Trapezoidal, Wiper
  • Cutting Speed 100-300 m/min (depending on material and tool)
  • Cutting Edge Design Sharp, Rounded, Double-edged, Single-edged
  • Feed Rate 0.1-0.5 mm/tooth (depending on material and process)
Other Attributes
  • Tool Holder Type Shell Mills, Face Mills, End Mills, Arbor Mills
  • Coolant Type Flood Cooling, Minimum Quantity Lubrication (MQL), Air Blast
  • Insert Material Tungsten Carbide, Cermet, Ceramic, Polycrystalline Diamond (PCD)
  • Insert Material Tungsten Carbide, Cermet, Ceramic, Polycrystalline Diamond (PCD)
  • Chipbreaker Type Positive, Negative, Flat, Serrated
Slider Image
Slider Thumb

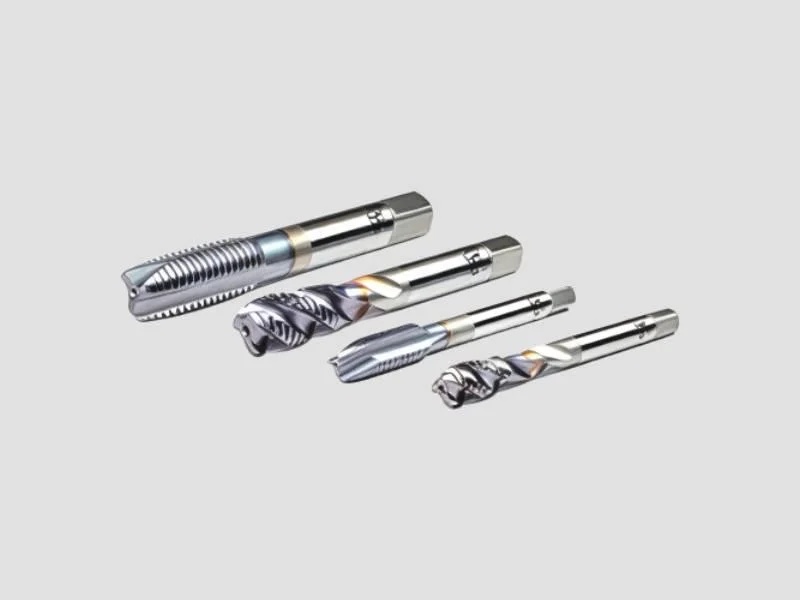
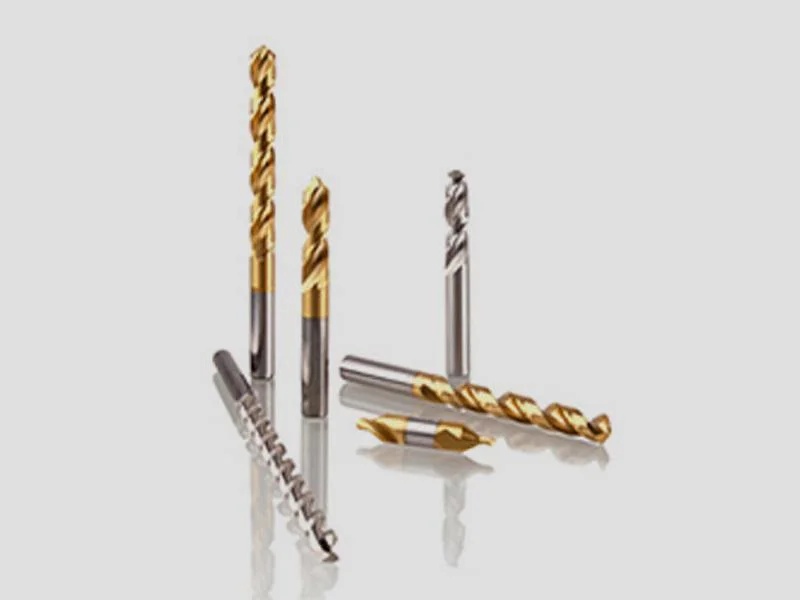
High-efficiency taps are also optimized for high cutting speeds, which reduce cycle times and increase overall productivity. Additionally, these taps offer superior wear resistance, providing a longer tool life and fewer tool changes, resulting in reduced downtime and cost savings. They are compatible with a range of cutting fluids, ensuring smooth operations and better surface finishes. The tapping capacity varies depending on the specific tool, but these taps are typically capable of handling both standard and large-diameter threads with consistent results. Their enhanced cutting performance makes them ideal for industries where precision and productivity are critical.

Cash,Cheque,Demand Draft,UPI, NEFT

Key Attributes
Industry-specific Attributes
  • Tapping Capacity M3 - M24 (metric), #0 - 1” (imperial)
  • Tool Geometry Spiral Point, Spiral Flute, Straight Flute
  • Cutting Speed 30-50 m/min (for HSS), 80-120 m/min (for Carbide)
  • Wear Resistance High (for TiN-coated taps), Very High (for TiAlN-coated taps)
  • Tool Life 500-2000 threads (depending on material and cutting conditions)
Other Attributes
  • Cutting Fluid Compatibility Water-based Coolants, Oil-based Coolants, Dry Tapping
  • Surface Finish Ra 0.8 μm, Ra 1.6 μm, Ra 3.2 μm (depending on the tap quality and material used)
  • Material HSS (High-Speed Steel), Carbide, Cobalt
  • Coating Type (Titanium Nitride), TiAlN (Titanium Aluminum Nitride), AlTiN (Aluminum Titanium Nitride)
Slider Image
Slider Thumb

The diameter of the face mill determines the width of the cut, and larger diameters are typically used for more significant, heavy-duty operations. Inserts come in various materials such as carbide, offering durability and heat resistance for extended tool life. The number of inserts influences the cutting stability and surface finish, as well as the feed rate and cutting speed. Face mills can be customized with different numbers of flutes to control chip removal and surface quality. Tool length and the type of coolant used can also impact the performance. Longer tools may lead to tool deflection, while the proper coolant ensures efficient heat management and chip evacuation. Face mills are widely used in industries like aerospace, automotive, and manufacturing for their ability to produce precise and smooth finishes.

Cash,Cheque,Demand Draft,UPI, NEFT

Key Attributes
Industry-specific Attributes
  • Diameter Determines the width of the cut and the amount of material removed per pass. Common sizes range from small (50mm) to large (500mm+)
  • Number of Inserts Typically varies from 3 to 12 or more inserts, depending on the size of the face mill and the required cutting performance.
  • Insert Material Common materials include carbide, ceramic, cermet, and high-speed steel (HSS), each suited to specific machining conditions such as hardness, cutting speed, and material type.
  • Insert Type Inserts may have different geometries, including square, round, or diamond shapes, which influence cutting forces, surface finish, and chip control.
Other Attributes
  • Cutting Speed The recommended cutting speed can range from 80 to 250 m/min, depending on the material being machined and the insert material.
  • Tool Length Face mills come in various lengths, with common lengths ranging from 50mm to 300mm. Longer tools may suffer from deflection and vibrations.
  • Number of Flutes Common face mills have 3 to 8 flutes, but the number may vary based on the cutting material and the surface finish requirements.
  • Tool Material Face mills are often made from high-strength steel, carbide, or other alloys. Steel provides strength, while carbide offers wear resistance and durability in high-speed operations.
Slider Image
Slider Thumb

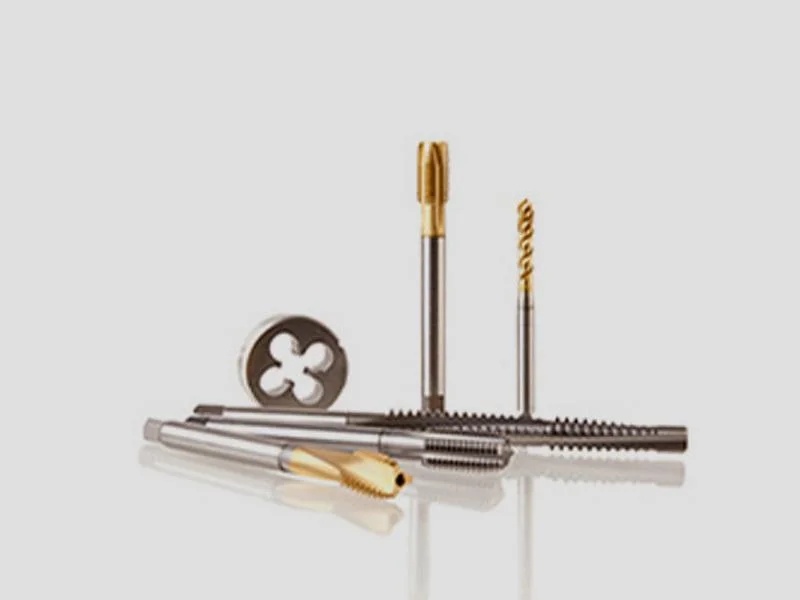
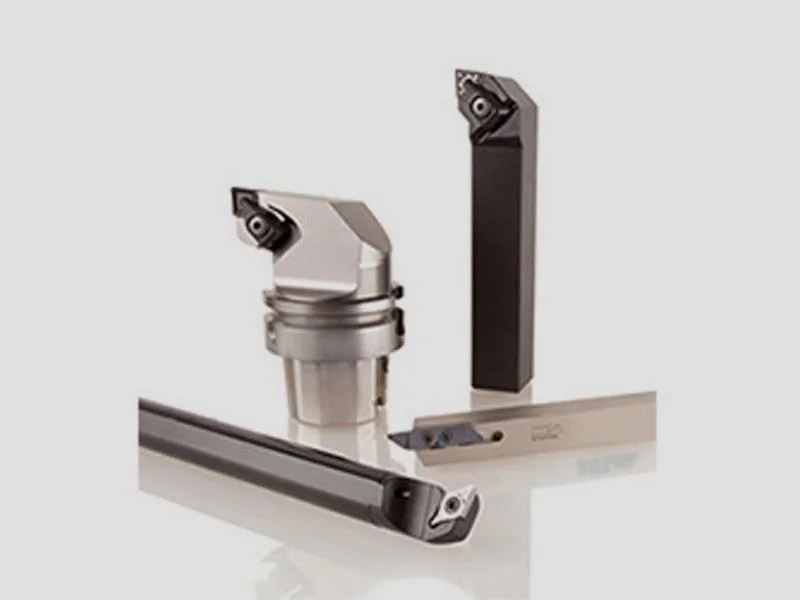
Threading tools also differ in the type of thread they can create—such as unified threads, metric threads, or tapered threads—making them versatile for various applications. The cutting edge design, tool life, and cooling methods all influence the tool’s performance, reducing the risk of overheating and ensuring precision during the cutting process. In terms of compatibility, threading tools must be chosen based on their compatibility with the tool holder and machine setup. Proper selection ensures optimum cutting parameters, such as speed and feed rate, to achieve the best results in terms of surface finish and thread accuracy.

Cash,Cheque,Demand Draft,UPI, NEFT

Key Attributes
Industry-specific Attributes
  • Material Composition High-speed steel (HSS), cobalt, carbide, or a combination, designed for high wear resistance and heat tolerance.
  • Thread Type Suitable for creating different thread forms such as UNC (Unified National Coarse), UNF (Unified National Fine), metric, BSPT (British Standard Pipe Tapered), and NPT (National Pipe Tapered).
  • Thread Size Range Can range from M1 to M100 (metric) or 0-80 to 2
  • Cutting Edge Geometry Includes straight, spiral, and combination flutes; features may include internal or external cutting edges for different threading applications.
  • Coating Type Common coatings include Titanium Nitride (TiN), Titanium Aluminum Nitride (TiAlN), and other wear-resistant coatings designed to reduce friction and enhance tool longevity.
Other Attributes
  • Flute Length Typically ranges from 1x to 3x the diameter of the tool, depending on the application and material being threaded.
  • Shank Size Threading tools usually have a shank diameter that ranges from 6mm to 20mm for hand tools, or larger for industrial tools.
  • Cutting Speed (Vc) Typically between 50 m/min to 200 m/min depending on the material, coating, and machine capability.
  • Feed Rate (f) Common feed rates range from 0.1 mm/rev to 0.5 mm/rev, depending on the material and threading tool type.